SLS vs FDM: Unit Cost Comparison for Mid-Volume Parts
SLS and FDM have different cost structures for mid-volume production. SLS often wins at higher volumes due to no support material and continuous batch processing. FDM can be cheaper at lower volumes but scales poorly. Choose based on part geometry and quantity.
- SLS unit costs drop faster than FDM as volume increases because it requires no support material.
- FDM remains competitive at lower volumes when material price and machine access are the main cost drivers.
- Build time and post-processing effort shift the cost balance between the two processes.
- Part geometry determines which process handles mid-range quantities more efficiently.
- Total cost includes material, machine time, post-processing, and waste, not just material price.
How the cost structure differs at mid-range volumes
Mid-volume production sits in the gap between one-off prototyping and high-volume injection molding. For polymer parts in this range, SLS and FDM represent two distinct approaches to cost control. The difference is not just the machine type. It is how each process converts material into finished parts.
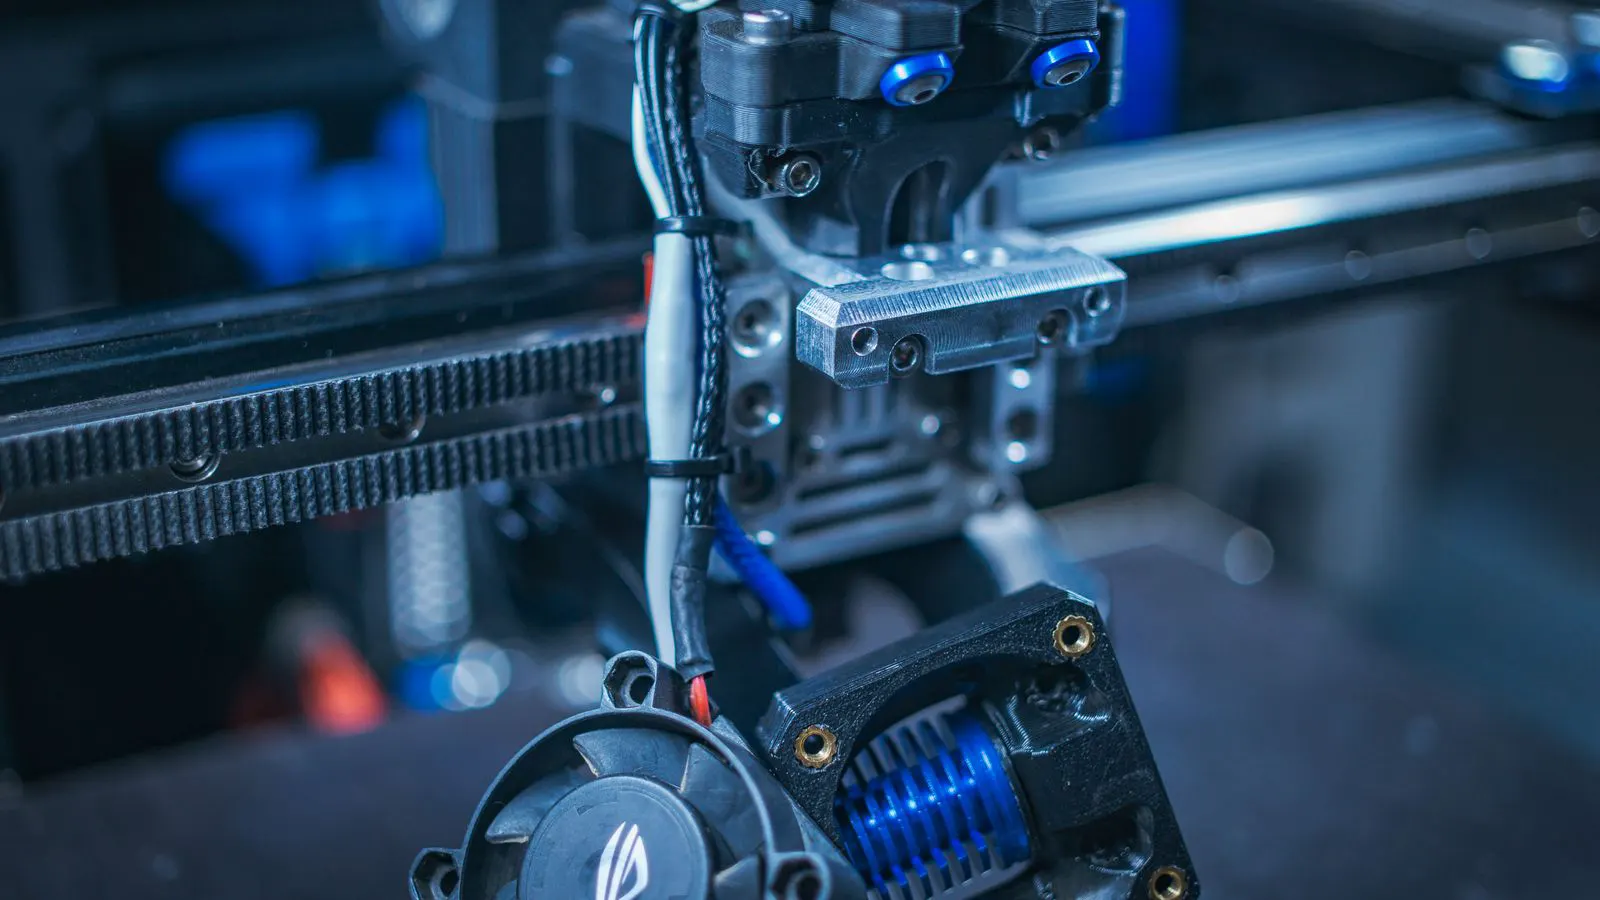
FDM builds parts by melting and extruding thermoplastic filaments. The material is laid down in layers. This method creates a physical part, but it also creates a lot of waste. Support structures, failed builds, and material that is removed during post-processing all add to the effective cost per part.
SLS uses a laser to sinter powdered polymer on a bed. The parts form from the powder, and the unused material is simply raked off and reused. There are no support structures. The entire build layer is used. This changes the cost curve. At low volumes, the machine time and material cost per part may be higher than FDM. As volume increases, SLS becomes more efficient because the cost of the build time spreads across more parts.
The material cost factor
Polymer AM pricing is rarely driven by material alone. Material is only one component of the unit cost.
FDM uses filaments, usually spooled in standard sizes. The material cost per kilogram is often lower than SLS powder. However, the effective cost per finished part depends on how much filament is used and how much is lost. A part that requires complex supports will consume extra material that is discarded.
SLS powder is generally more expensive per kilogram than FDM filament. The price difference reflects the processing requirements for the powder. But the material efficiency is higher. The powder is used in the build, and the residual powder is recycled. The yield rate is significantly better than FDM.
A buyer evaluating polymer AM pricing must look at the cost per usable part, not the cost per kilogram. A kilogram of SLS powder may cost more, but it produces more finished parts per kilogram than the same weight of FDM filament, especially for complex geometries.
Unit cost comparison table
The table below summarizes the typical cost drivers for each process at mid-volume production levels. It is not a price list. Prices vary by region, supplier, and machine type. The structure of the cost is what matters.
| Option | Best for | Limitations |
|---|---|---|
| FDM | Low to moderate volumes, simple parts, rapid prototyping | High support material waste, longer build times for complex shapes |
| SLS | Mid to high volumes, complex geometries, functional parts | Higher powder cost, larger machine footprint, longer post-processing |
| MJF | High volumes, high throughput, consistent quality | High machine cost, limited material availability |
| DLP | Fine detail, high volume, small parts | Material cost, build volume limitations, post-curing time |
Build time and machine utilization
Machine time is a major cost component in both processes.
FDM machines have a fixed build volume. A part that fits in a small corner of the bed still uses the same machine time as a part that fills the entire bed. The machine runs until the part is done. There is no way to run multiple different parts in the same build volume without compromising quality or structural integrity. This leads to a lot of idle space.
SLS machines have a larger build volume, and the entire bed is used for a single build layer. The laser scans the entire bed to sinter the powder. This means the build time is determined by the height of the part and the scan rate, not the surface area. A large part and a small part of the same height take roughly the same time. This is a key difference. It makes SLS more efficient when the build volume is not fully use in FDM.
For mid-volume production, this difference in utilization changes the unit cost. If you are producing 500 parts of a specific size, FDM will likely require multiple builds. SLS can often fit all 500 parts in one or two builds. The machine time per part drops dramatically.
Post-processing and finishing costs
The cost of getting a part from the machine to a usable state is often underestimated.
FDM parts require the removal of support material. This is a labor-intensive process. It can be done by hand or with specialized tools. The time required depends on the complexity of the part and the type of support used. The rough surface finish of FDM parts may also require sanding or other finishing to meet dimensional or aesthetic standards.
SLS parts come out of the machine in a state of the powder. The surface is matte and porous. It is usually not suitable for direct use in many applications. Post-processing includes cleaning the powder, which is often done in a fluidized bed or with compressed air. The parts are then typically sintered again to reduce porosity, or coated with a primer. The surface finish of SLS parts is often smoother than FDM, but it still requires finishing for most functional applications.
The labor cost for post-processing can be significant. It is not just about the machine time. It is about the hands-on work required to make the part usable.
When to pick SLS for cost efficiency
SLS is the better choice when the volume is high enough to justify the machine time and material cost. It is the better choice when the part geometry is complex.
A part with overhangs, internal channels, or thin walls will take a long time to print in FDM. The supports required will consume a lot of material. The post-processing will take a lot of time. The effective unit cost will be high.
In SLS, the same part can be printed without supports. The build time is the same as a simple part of the same height. The material is used efficiently. The post-processing is standardized.
If you are producing 100 to 1000 parts per month, SLS often becomes the lower cost option. The unit cost drops as the volume increases. The machine is use more effectively. The waste is minimized.
When to pick FDM for cost efficiency
FDM is the better choice when the volume is low. If you are producing 10 to 50 parts, the cost of a single SLS build may be higher than running a few FDM builds.
FDM is also the better choice when the part is simple. A flat plate or a simple bracket does not need supports. The material is used efficiently. The build time is short. The post-processing is minimal.
FDM is also the better choice when the material properties are critical. There are specific FDM filaments that offer high heat resistance or chemical resistance. SLS powders have their own range, but the selection may be different.
If you are producing a small batch of a simple part, FDM is often the lower cost option. The machine time is short. The material cost is low. The post-processing is minimal.
How to calculate your own unit cost
To determine which process is cheaper for your specific parts, you need to calculate the unit cost yourself.
- Identify the part geometry and the required finish.
- Determine the material properties needed.
- Estimate the build volume for both FDM and SLS.
- Estimate the machine time for both processes.
- Estimate the material usage for both processes.
- Estimate the post-processing time and labor cost.
- Add the cost of the machine depreciation or the cost of a service provider.
- Divide the total cost by the number of parts.
This calculation is not an exact science. It is an estimate. But it will give you a good idea of which process is cheaper for your specific case.
The most common mistake is to look only at the material cost per kilogram. A buyer must look at the total cost per part. The build time, the post-processing, and the machine utilization are all part of the cost.
Final thoughts
The choice between SLS and FDM for mid-volume production is not a simple one. It depends on the part, the volume, and the specific cost structure of your operation.
SLS is generally more cost-effective at higher volumes and for complex parts. FDM is generally more cost-effective at lower volumes and for simple parts.
By understanding the cost structure of each process, you can make an informed decision. You can choose the process that gives you the best value for your specific production needs.
Frequently asked questions
Is SLS always more expensive than FDM per kilogram of material?
Yes, SLS powder is generally more expensive per kilogram than FDM filament. However, the effective cost per finished part can be lower for SLS due to higher material efficiency and less waste.
How does part complexity affect the cost comparison?
Complex parts with overhangs and internal features are much more expensive in FDM because they require support material and longer build times. In SLS, the build time is largely independent of the part's surface area, so complex parts do not incur a significant cost penalty compared to simple parts.
Can I produce 500 parts in a single FDM build?
It depends on the size of the parts and the build volume of the machine. If the parts are small, you can fit many in a single build. However, the build time will be the same as for a single large part of the same height. In SLS, you can also fit many parts in a single build, but the build time is also determined by the height.
What is the main advantage of SLS for mid-volume production?
The main advantage is the ability to produce many parts in a single build without support material. This leads to a lower unit cost as the volume increases, especially for complex geometries.
How long does post-processing take for SLS parts?
Post-processing for SLS parts typically involves cleaning the powder, sintering or coating, and possibly sanding or machining. The time required depends on the number of parts and the desired finish. It is generally less labor-intensive than removing supports from FDM parts.